
Cap Embroidery Digitizing: The Complete Guide (2026)
Embroidery on caps is one of the most challenging tasks in commercial decoration, and running a standard flat-garment file on a structured hat almost always leads to puckered seams, misaligned borders, and broken threads. Because caps are stretched across a curved cylinder driver, the fabric moves and shifts completely differently than a flat t-shirt or polo. Achieving crisp lettering and clean registration on a hat requires a specialized digitizing strategy, including center-out and bottom-up pathing, increased pull compensation, and proper underlay control. This complete 2026 guide breaks down the exact settings, pathing rules, and troubleshooting fixes you need to digitize flawless cap embroidery every single time.
In This Guide
- What Is Cap Embroidery Digitizing?
- Why Caps Are Harder to Digitize Than Flat Garments
- The Cap Digitizing Workflow, Step by Step
- Structured vs. Unstructured Caps
- Fixing Off-Center Logos
- Stopping Puckering and Thread Breaks
- Stitch Density and Pull Compensation Chart
- Underlay Selection by Element
- Needle and Thread Selection
- 3D Puff Cap Embroidery
- Registration Gaps and Flagging
- Troubleshooting Matrix
- File Formats and Machine Compatibility
- Pre-Production Checklist
- Cost and Turnaround
- FAQs
What Is Cap Embroidery Digitizing?
Cap embroidery digitizing is the process of converting artwork into a stitch file DST, .PES, or .EMB built specifically for a cap frame driver rather than a flat hoop. The machine holds the cap on a curved, cylindrical frame and rotates it under the needle instead of moving a flat platen in two directions. That single mechanical difference changes almost every setting in the file: pathing order, underlay type, stitch density, and pull compensation all have to account for the crown's curvature, the rigid front panel (buckram), and the vertical center seam that most logos sit directly on top of.
A file digitized for a t-shirt or polo a flat-garment file is not a cap file. Running one on a cap frame is the single most common cause of the off-center logos, puckering, and thread breaks covered in this guide.
Why Caps Are Harder to Digitize Than Flat Garments
| Factor | Flat Garment Digitizing | Cap Digitizing |
|---|---|---|
| Stitching surface | Flat, stable platen | Curved cylinder, 270°+ rotation under the needle |
| Fabric backing | Soft, flexible | Rigid buckram (structured) or unsupported twill (unstructured) |
| Center seam | None to work around | Vertical seam runs through most logos |
| Pull compensation | 0.15–0.20 mm | 0.30–0.40 mm (up to 0.45 mm on wide satin) |
| Stitch spacing | 0.35–0.40 mm | 0.42–0.45 mm |
| Digitizing order | Any logical sequence | Center-out, bottom-up (mandatory) |
| Needle | Standard sharp | SAN 6 / DBxK5, sharp or SES ballpoint, titanium-coated preferred |
The Cap Digitizing Workflow, Step by Step
Step 1 — Prep and simplify the artwork. Convert raster logos to clean vector paths. Remove gradients and fine detail that can't survive a 5 mm text minimum or a 1.0 mm satin column caps punish over-detailed artwork more than flat garments do.
Step 2 — Build the cap frame profile in your software. Match the frame's curvature radius to the actual cap sample on your machine, not a generic default. A mismatched radius is the single biggest cause of registration drift between the digitized preview and the real stitch-out.
Step 3 — Set the pathing order: center-out, bottom-up. Start at the vertical center seam and digitize outward left, then right so push forces stay symmetrical. Sequence lower elements before upper ones so fabric waves get pushed up toward the crown instead of bunching at the seam.
Step 4 — Build underlay before top stitches. Choose the underlay type by element (see the underlay table) and inset it 0.3–0.4 mm inside the final stitch border so it never peeks out from under top stitching.
Step 5 — Set stitch density per element. Standard cap density runs 0.40–0.42 mm spacing on structured caps and 0.42–0.45 mm on unstructured caps 10–15% lower than a flat-garment file to reduce needle drag and heat on stiff fabric.
Step 6 — Apply pull compensation. Raise compensation to 0.30–0.40 mm on satin columns (0.45 mm on columns wider than 6 mm). Over-compensate along the pull axis and under-compensate along the push axis to keep letterforms and logo edges geometrically true.
Step 7 — Digitize small text last, with its own rules. Never go below a 1.0 mm column width (1.2 mm preferred), keep text at 5 mm tall minimum, and use center-walk underlay only a heavy edge-walk underlay is what makes small lettering fill in and go illegible.
Step 8 — Add 3D puff elements, if the design calls for them. Digitize sharp, triangular capping stitches at every open end so the needle slices the foam cleanly instead of tearing it, and raise density 50–100% over the foam (see the 3D puff section).
Step 9 — Sequence colors and trims to cut thread breaks. Group same-color elements together and minimize jump stitches across the center seam, where tension is least forgiving.
Step 10 — Run a real sew-out test on an actual cap, not a flat scrap. A test on flat fabric will not reveal cap-specific pull, flagging, or registration problems. Measure the logo against its intended placement and check both edges of the center seam.
Step 11 — Adjust, finalize, and export. Correct any drift the test revealed, then export to .DST (Tajima), .PES (Brother), or .EMB (Wilcom) as needed, and keep a native/editable backup format for future edits.
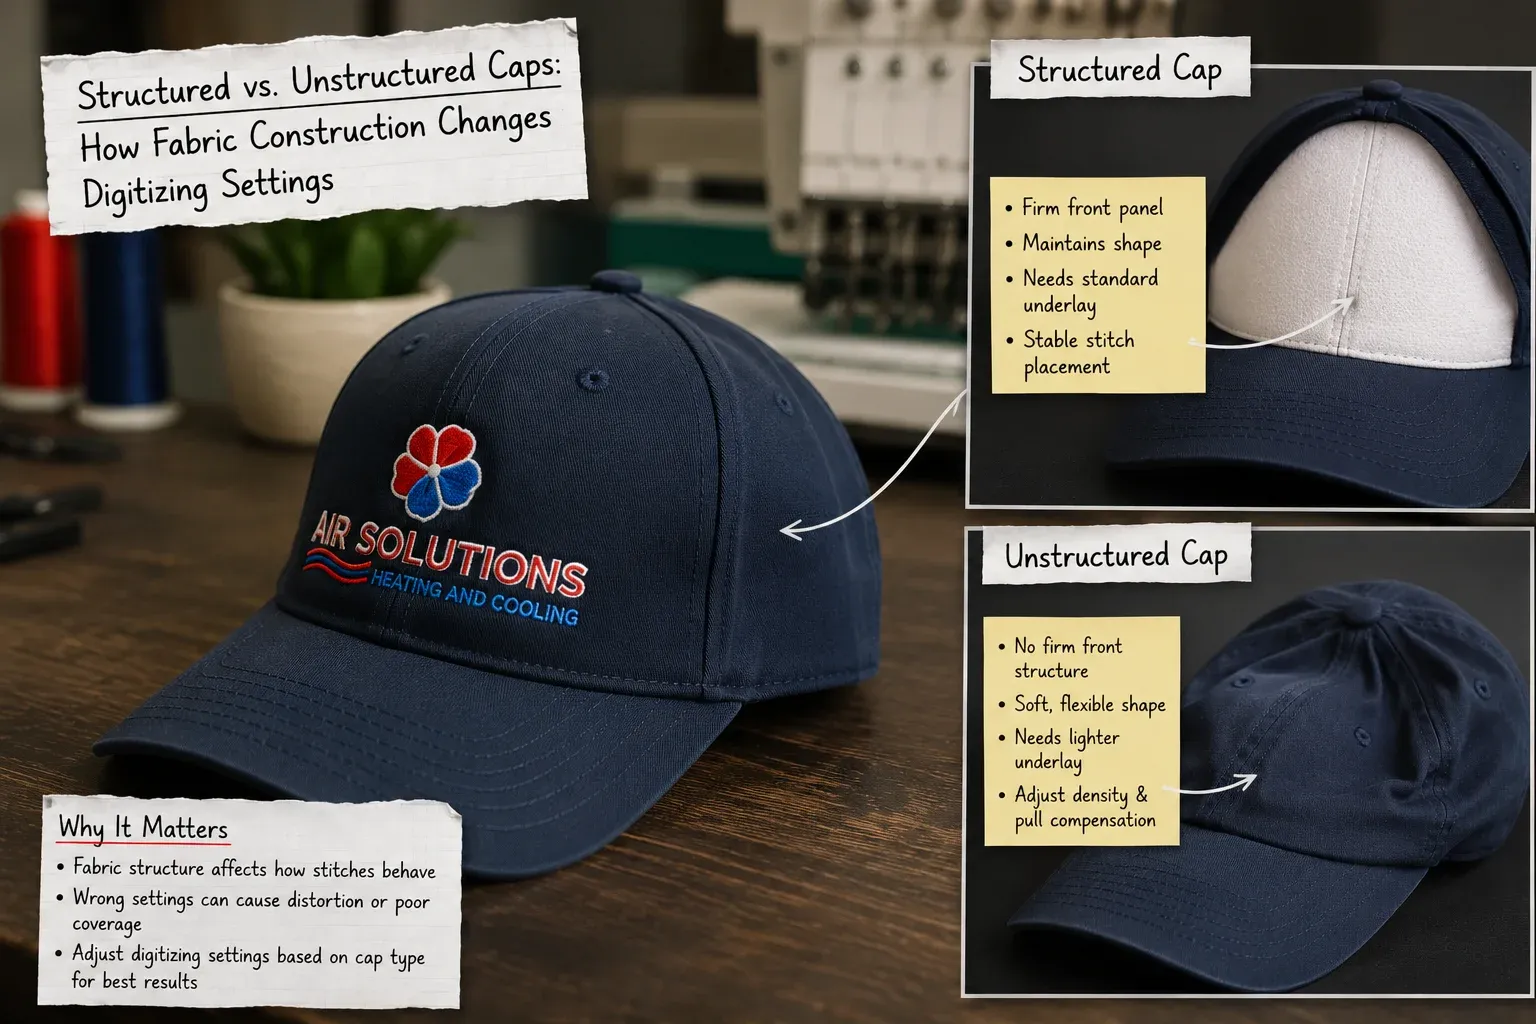
Structured vs. Unstructured Caps: How Fabric Construction Changes Your Settings
| Feature | Structured Caps | Unstructured Caps |
|---|---|---|
| Front panel | Heavy buckram lining, stiff and self-supporting | Soft cotton twill or canvas, no internal stiffener |
| Pull compensation | Standard cap range (+0.20–0.30 mm) | High (+0.35–0.50 mm) |
| Underlay strategy | Light edge-walk or center-walk | Heavy grid/tatami or double zig-zag |
| Stitch density | 0.40–0.42 mm spacing | 0.42–0.45 mm spacing |
On unstructured caps, the underlay has to do the job buckram does on a structured cap it's the mesh foundation that keeps fabric from moving under the needle, so treat it as non-negotiable rather than optional.
Fixing Off-Center Logos
Root cause: rotational torque. As the cap frame driver rotates the cylinder and the needle bar moves horizontally, the combined forces push fabric across the curved crown enough to shift a logo 2–5 mm from its intended position if the file isn't built to counter it.
Fix:
- Digitize center-out from the vertical seam, not left-to-right across the whole design.
- Keep cap-frame tension uniform along the sweatband strap before you start the run.
- Anchor heavy elements with a lock stitch along the center seam before stitching them.
Stopping Puckering and Thread Breaks on Curved Surfaces
Root cause: dynamic drag and needle heat. Needle friction against stiff cap fabric ripples the surface and generates enough heat to shred or break thread especially on dense fill areas.
Fix:
- Lower satin and fill density 10–15% (stitch spacing 0.42–0.45 mm instead of a flat-garment 0.38 mm).
- Use heavy-weight tearaway backing (2.5–3.0 oz) formulated for cap drivers.
- Switch to SAN 6 or DBxK5 needles, size 75/11 or 80/12, sharp or SES ballpoint tip; titanium-coated needles cut friction-related heat further.
Stitch Density and Pull Compensation Quick-Reference Chart
| Element | Stitch Spacing | Pull Compensation |
|---|---|---|
| Standard satin column (under 6 mm) | 0.40–0.42 mm | 0.30–0.40 mm |
| Wide satin column (over 6 mm) | 0.40–0.42 mm | up to 0.45 mm |
| Fill/tatami areas | 0.42–0.45 mm | 0.25–0.35 mm |
| Small lettering (under 5 mm tall) | 0.42–0.48 mm | 0.15–0.20 mm (minimal — over-compensation blurs letterforms) |
| 3D puff satin over foam | 0.20–0.22 mm | 0.35–0.45 mm |
Underlay Selection by Element Type
| Element Type | Primary Underlay | Secondary Underlay |
|---|---|---|
| Narrow satins | Center-walk | None |
| Medium/wide satins | Edge-walk | Zig-zag |
| Large fills | Tatami/mesh grid | Edge-walk outline |
| Micro text | Center-walk (light) | None |
Run open-grid or light tatami underlay at a 90-degree angle to the main fill direction, and keep every underlay path inset 0.3–0.4 mm inside the final stitch border so movement never exposes it.
Needle and Thread Selection for Caps
| Cap Element | Needle | Thread |
|---|---|---|
| Standard structured cap, general stitching | SAN 6 / DBxK5, 75/11 or 80/12, sharp/SES hybrid tip | 40-weight polyester or rayon |
| Titanium-coated (high-volume production runs) | Titanium SAN 6, 75/11 or 80/12 | 40-weight polyester |
| Small lettering under 5 mm | 65/9, sharp | 60-weight polyester |
| 3D puff over foam | 75/11–80/12, sharp | 40-weight polyester (higher tensile strength through foam) |
3D Puff Cap Embroidery Without Foam Peeking Through
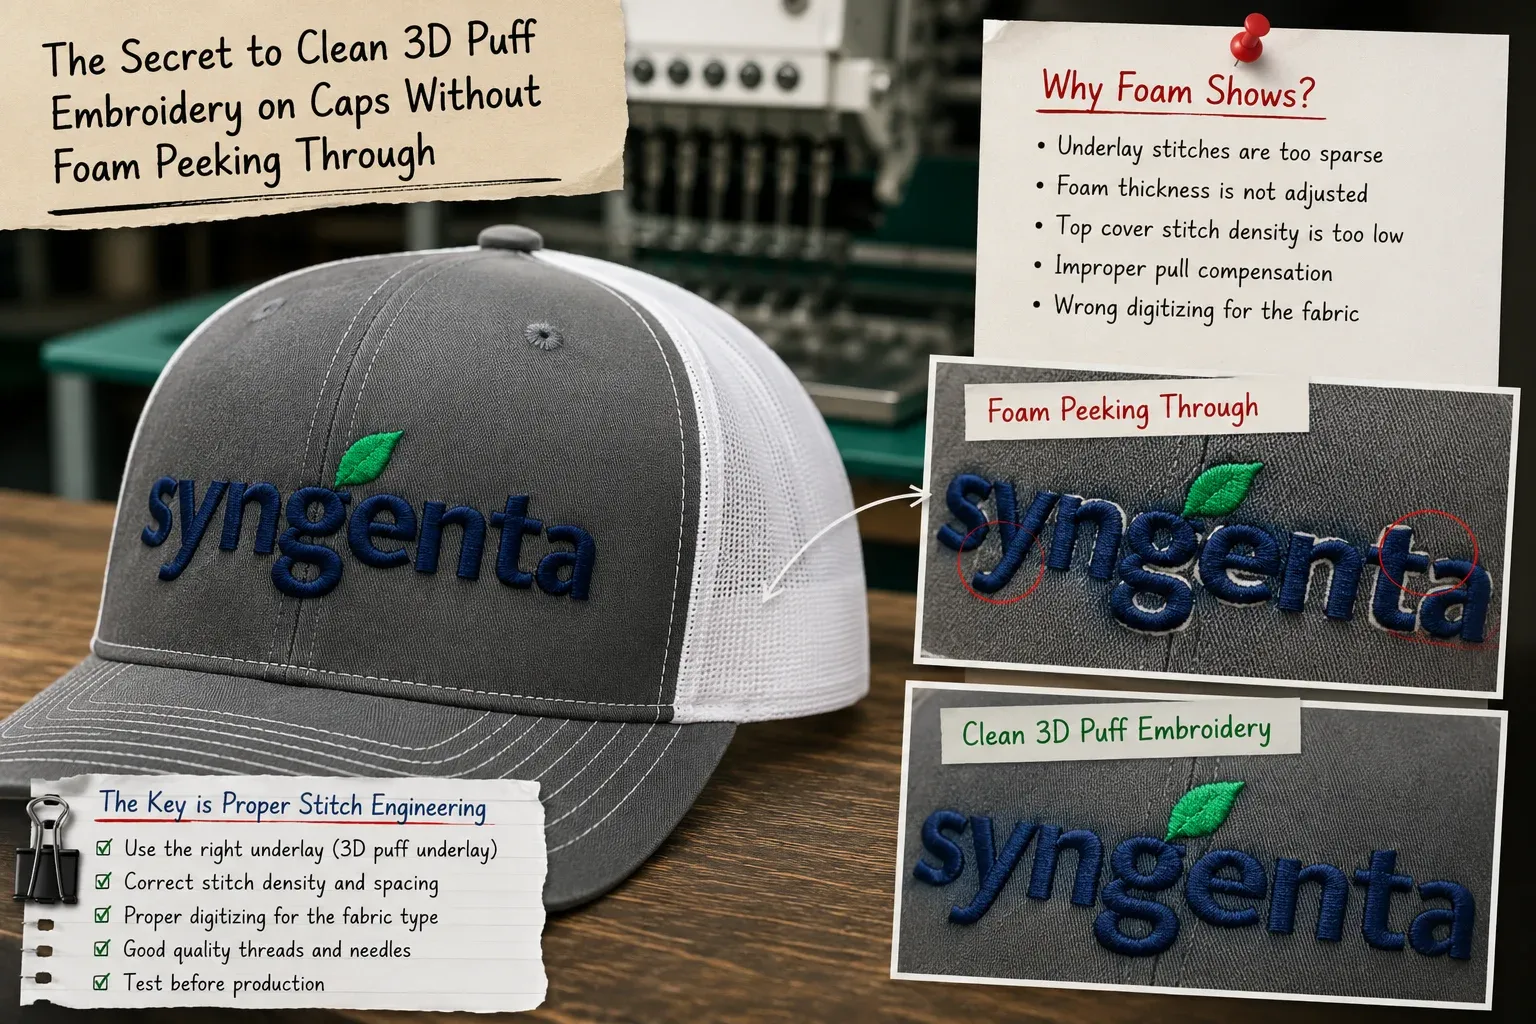
- Increase density 50–100% over foam drop spacing from a flat 0.40 mm down to 0.20–0.22 mm.
- Digitize sharp, triangular capping stitches at every open end so the needle slices foam cleanly instead of tearing it.
- Use high-density 2–3 mm EVA foam; soft craft foam tears unevenly under the needle.
- Never run underlay over the foam itself underlay only the flat sections around it.
A heat gun, used carefully after stitching, shrinks any foam that still protrudes past the stitch edge.
Registration Gaps and Flagging: Two More Cap-Specific Failures
Registration gaps happen when fabric push/pull is unsynchronized during curved-surface stitching, so an outline sews onto bare fabric instead of overlapping the fill it's meant to border. Fix it by sewing fill and outline in the same sequence without long gaps between them, extending fill 0.4–0.6 mm underneath the outline's satin border, and avoiding outline directions that run perpendicular to the fill direction on unstable fabric.
Flagging is the vertical bounce of cap fabric during needle retraction it causes skipped stitches, loops, bird-nesting, and thread breaks. Fix it by setting the presser foot slightly lower than your flat-garment setting (firm contact, no shine on the fabric), balancing bobbin tension at 22–25 grams, running top thread tension firmer than flat settings (110–130 grams), and confirming less than 1 mm of play between the cap frame driver ring and the machine arm.
Troubleshooting Matrix
| Symptom | Most Likely Cause | Fix |
|---|---|---|
| Logo shifts off-center during stitching | Left-to-right pathing instead of center-out | Rebuild pathing from the center seam outward |
| Puckering on the crown or front panel | Density too high for cap fabric / wrong needle | Drop density 10–15%; switch to SAN 6/DBxK5 |
| Thread breaks mid-run | Needle heat buildup, wrong needle size | Titanium-coated needle; verify 75/11–80/12 |
| Small text fills in and blurs | Edge-walk underlay under micro text | Switch to center-walk-only underlay, 1.0 mm+ columns |
| Foam shows through 3D puff | Density too low over foam, dull capping stitches | Raise density 50–100%; add sharp triangular capping stitches |
| Gaps between outline and fill | Fill and outline sewn out of sequence | Sew in the same pass; extend fill 0.4–0.6 mm under outline |
| Skipped stitches, bird-nesting | Flagging presser foot or tension too loose | Lower presser foot slightly; raise top tension to 110–130 g |
| Logo distorted or stretched | Insufficient pull compensation for cap frame curvature | Raise compensation to 0.30–0.40 mm (0.45 mm on wide satin) |
File Formats and Machine Compatibility
| Format | Common Machine Brands | Notes |
|---|---|---|
| .DST | Tajima and most commercial multi-head machines | Industry-standard format for production shops |
| .PES | Brother, Babylock | Consumer and light-commercial single-head machines |
| .EMB | Wilcom | Native editable format keep as your backup/edit copy |
Ask your digitizer for the production format your machine reads plus one editable backup format, so future resizes or edits don't require a full re-digitize.
Pre-Production Checklist
Before a cap file goes to the production floor, confirm:
- ✅ Pathing follows center-out and bottom-up order
- ✅ Pull compensation raised to at least 0.30–0.40 mm
- ✅ Overall stitch density lowered 10–15% from flat-garment settings
- ✅ Small text uses center-walk underlay only, with 1.0 mm+ column widths
- ✅ Needle confirmed as 75/11 or 80/12, SAN 6/DBxK5, sharp or SES
- ✅ Presser foot height set to prevent flagging
- ✅ A real sew-out test has been run on an actual cap sample, not flat scrap
Cost and Turnaround: What to Expect From Professional Cap Digitizing
Cap digitizing typically costs more than a flat-garment file of the same stitch count because of the extra setup cap frame profiling, pull compensation tuning, and a physical sew-out test add time a flat file doesn't need. Turnaround for a standard commercial cap logo usually runs 12–24 hours with a professional digitizer; rush service is available for time-sensitive production runs. Exact pricing depends on stitch count, 3D puff elements, and lettering complexity see current rates on the pricing page.
Shops that digitize caps in-house without cap-frame-specific settings tend to lose more time to re-runs, thread breaks, and hooping fixes than they save on digitizing fees which is the core reason commercial shops outsource cap files to a specialist rather than adapting a flat-garment file.
Frequently Asked Questions (FAQs)
Can I use the same digitizing file for flat shirts and caps?
No. A flat-garment file lacks the pull compensation (0.30–0.40 mm), center-out pathing, and cap-specific underlay a curved cap frame needs. Running it on a cap produces off-center logos and registration gaps.
Why does my cap embroidery shift to the right side during stitching?
Left-to-right pathing pushes fabric ahead of the needle as it crosses the crown. Center-out pathing starting at the vertical seam and working outward both directions keeps the push forces symmetrical and prevents the shift.
What needle size and type is best for structured caps?
A 75/11 or 80/12 SAN 6/DBxK5 needle with a sharp or light ballpoint (SES) tip. Titanium-coated sharp needles cut cleanly through buckram without deflecting off the stiff backing.
How do I prevent foam from showing through 3D puff cap embroidery?
Increase satin density 50–100% (0.20–0.22 mm spacing) over the foam, digitize sharp capping stitches at every column end to slice the foam cleanly, and never run underlay over the foam area itself.
Why does small lettering on caps fill in and look messy?
Standard density and a heavy edge-walk underlay make small text illegible. For text under 5 mm tall, use center-walk underlay only, keep column widths at 1.0 mm minimum, open density to 0.42–0.48 mm spacing, and consider 60-weight thread with a 65/9 needle.
What file format do I need for my embroidery machine?
Tajima and most commercial multi-head machines read .DST. Brother and Babylock single-head machines read .PES. Wilcom uses .EMB as its native editable format. Most professional digitizers deliver the production format plus an editable backup on request.
How long does professional cap digitizing take?
Standard turnaround runs 12–24 hours for a typical commercial logo. Rush options are usually available for time-sensitive orders check with your digitizer before submitting a deadline-critical job.
How many stitches does a typical cap logo need?
Most commercial cap logos run 5,000–12,000 stitches depending on size, lettering, and whether 3D puff elements are included. Fewer, better-placed stitches generally outperform an over-digitized file on a curved surface.
Should I digitize caps in-house or outsource to a professional digitizer?
If your shop runs cap orders regularly and has a dedicated cap-frame-trained digitizer, in-house can work. Most commercial shops outsource cap files specifically because cap-frame settings differ enough from flat digitizing that a general-purpose file causes costly re-runs outsourcing to a specialist is usually cheaper than the thread, backing, and downtime lost to trial-and-error.
Keith Blair
Senior Quality Control (HOD)
As the Head of Quality Control at Sassy Digitizing, Keith brings over 12 years of hands-on commercial embroidery experience to the table. He is our resident problem-solver, specializing in the technical nuances of stitch density, pull compensation, and complex digitizing. When he's not establishing quality standards for 3D puff and appliqué, you'll find him perfecting the art of small lettering to ensure every stitch counts.
Expertise:
Related Articles
How to Convert PNG to DST: A Complete Guide to Embroidery File Conversion
Discover how to turn flat PNG images into production-ready DST embroidery files for commercial machines like Tajima, Bar…
Brother PE800 & SE1900: A Beginner's Guide to Using Your Embroidery Machine
Get started with your Brother PE800 or SE1900 embroidery machine with this easy beginner’s guide. From understanding mac…
Beginner’s Guide to Small Lettering & Monogram Digitizing: Precision, Density, and Pathing Secrets
Learn how to digitize crisp, readable micro-text and monograms down to 3 mm with this complete technical guide. From adj…